Heavy-Duty Industrial Storage & Racking Systems
Engineered for high structural load capacity, cold-chain longevity, and maximum spatial efficiency in global distribution hubs.
Whitepaper: Strategic Engineering & Metallurgy in Modern Industrial Racking
In the evolving landscape of global logistics, material handling efficiency is directly tethered to spatial density and structural integrity. Selecting an enterprise-grade China wholesale industrial racks for storage supplier and exporter requires an acute understanding of structural engineering dynamics, material yield strengths, and seismic resilience standards. Racking systems are no longer passive steel frames; they are dynamically loaded load-bearing infrastructures engineered to survive cyclic mechanical stress, forklift impact loads, and thermal acceleration.
1. Structural Steel Metallurgy & FEA Analysis
High-capacity storage systems manufactured in our China production facilities utilize high-tensile cold-rolled steel grades, predominantly Q235B and Q355B (equivalent to SS400 and S355JR under European specifications). The structural safety of every column section and beam connector relies on advanced Finite Element Analysis (FEA) modeling to simulate multi-directional vector forces under full loading conditions.
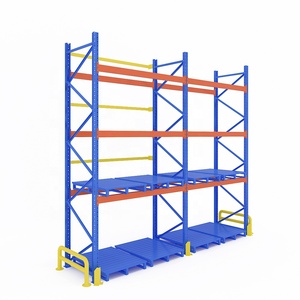
- Upright Profiles: Cold-rolled omega profiles featuring continuous 11-fold geometry optimize section modulus and torsional rigidity while mitigating buckling modes under static compression.
- Beam Connectors: Heavy-duty drop-in slot connectors engineered with 3, 4, or 5-hook structural teeth ensure positive engagement with the upright punching pattern (50mm or 75mm pitch), incorporating automated safety lock pins with high shear resistance.
- Surface Finishes: Advanced electrostatic epoxy-polyester powder coating (60–90 micron thickness) or hot-dip galvanizing (HDG) per ISO 1461 standards guarantees superior corrosion immunity in humid port facilities and cold storage (-30°C) operations.
2. Seismic-Ready Design Standards (NCh2369, RMI, & FEM 10.2.02)
Global logistics hubs situated in active seismic zones require storage systems compliant with international structural codes. Our engineering team incorporates site-specific dynamic response spectrum analyses, adhering strictly to global standards:
- FEM 10.2.02 / EN 15512: European structural standards governing cold-formed steel racking design, deflection limits ($L/200$), and safety factors ($S_f = 1.65$).
- RMI (ANSI MH16.1): North American Specification for the Design, Testing, and Utilization of Industrial Steel Storage Racking.
- Seismic Engineering (NCh2369 / ASCE 7): Heavy-duty structural baseplates with double-anchor expansions, heavy frame bracing ratios, and anti-seismic top ties engineered to withstand high peak ground acceleration ($PGA$).
Comprehensive Racking System Categories
Tailored storage architectures engineered for ambient, cold chain, chemical, and automated fulfillment operations.
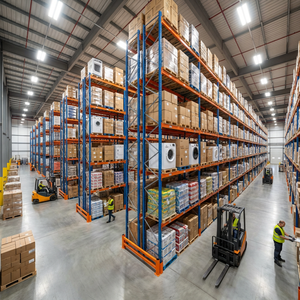
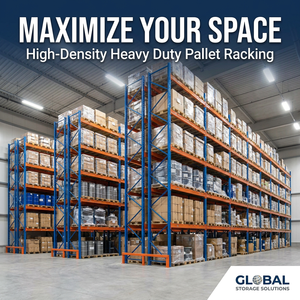
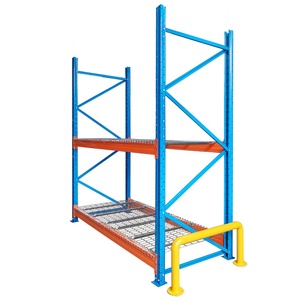
Selective Pallet Racking
Provides 100% direct pallet selectivity and effortless adjustment. Designed for high-turnover warehouses managing diverse SKU profiles, compatible with all forklift truck types.
Drive-In & Push-Back Racks
High-density storage utilizing LIFO or FIFO principle. Eliminates operating aisles to maximize floor space utilization up to 85%, ideal for cold storage and homogeneous goods.
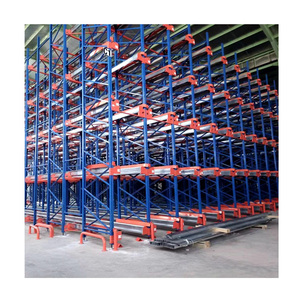
Radio Shuttle Automated Racks
Semi-automated deep-lane storage system utilizing self-powered lithium shuttle carts controlled via RF remote or WMS interface, drastically cutting forklift travel time and labor costs.
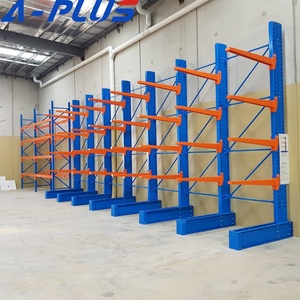
Heavy-Duty Cantilever Racks
Unobstructed front column design ideal for storing long, bulky materials like steel pipes, timber, copper bars, aluminum extrusions, and heavy machinery parts.
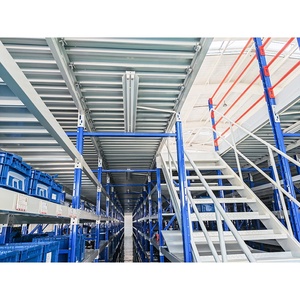
Warehouse Mezzanine Platforms
Multi-tier steel structure platforms that double or triple usable overhead floor space without expanding building footprints. Supports heavy unit loads up to 1,500 kg/m².
E-Commerce Multi-Tier Pick Modules
Integrated high-speed order fulfillment structures combining carton flow tracks, belt conveyors, and modular shelving for ultra-fast item picking and inventory turnover.
Future Sourcing Trends: Strategic 2025–2030 B2B Procurement Insights
As supply chains modernize, global procurement managers purchasing industrial racking from China exporters are shifting from basic purchase price considerations to Total Cost of Ownership (TCO), carbon intensity, and system intelligence. Understanding these micro- and macro-trends is crucial for high-return warehouse capital expenditure (CapEx).
Trend 1: ASRS Integration and Autonomous Mobile Robot (AMR) Readiness
Traditional static storage is rapidly integrating with automated material handling equipment. Modern industrial racking must now be manufactured with strict structural tolerances ($\pm 1.0\text{mm}$ frame alignment) to allow smooth operation of Automated Storage and Retrieval Systems (ASRS), AGVs, and AMRs. Beam profiles are fitted with optical sensor cutouts and barcode positioning strips for automated warehouse management software (WMS) tracking.
Trend 2: Sustainable "Green Steel" & Reduced Carbon Footprint Logistics
Global ESG mandates require suppliers to offer low-carbon industrial storage systems. China's top storage manufacturers are adopting electric arc furnace (EAF) recycled steel, eco-friendly solvent-free powder coatings, and zero-waste manufacturing processes. Optimized structural beam designs reduce raw material consumption while maintaining high load capacities, directly lowering shipping container weight and ocean freight carbon emissions.
Trend 3: Cold-Chain Logistics Expansion & Corrosion Resistance Innovation
The global surge in fresh produce, pharmaceutical, and frozen food logistics has escalated the demand for storage systems engineered for harsh sub-zero temperatures (-30°C). Cold storage environment causes steel embrittlement and severe condensation corrosion. Leading Chinese exporters are expanding pre-galvanized and hot-dip galvanized racking production lines to deliver self-healing zinc coatings that resist rust and ice formation for decades.
Why Partner With Us: Direct Factory Engineering Advantage
As a premiere China wholesale industrial racks for storage supplier & exporter, we combine state-of-the-art automated manufacturing with deeply experienced structural engineering services. We handle the full project lifecycle—from initial CAD site layout modeling to global logistics delivery and technical installation support.
Precision CNC Roll-Forming & Robotic Welding
Our manufacturing facility houses automated continuous roll-forming lines, laser punching units, and multi-axis Panasonic robotic welding stations ensuring seamless joint strength and zero dimensional deviation across long production runs.
Comprehensive QA/QC Laboratory Testing
Every batch undergoes tensile yield tests, salt spray corrosion testing (500+ hours ASTM B117), weld ultrasonic flaw detection, and full-scale hydraulic crush load testing to guarantee complete compliance with agreed specifications.
Turnkey Customization (OEM & ODM Services)
Whether you require custom upright color matching, specific frame depths, specialized seismic floor anchor plates, or OEM branded packaging, our engineering team custom-tailors racking specs to your precise operational parameters.
Optimized Global Export Logistics
We specialize in maximized 40ft HQ container packing algorithms. Component bundling, custom steel pallet cradles, and protective moisture barrier wrapping ensure safe sea transit and zero rust damage upon arrival at destination ports.
Frequently Asked Questions (FAQ)
Technical and procurement insights for procurement managers, logistics engineers, and warehouse operators.
How do I choose between Q235B and Q355B steel for industrial pallet racking?
Are Chinese industrial racking systems compliant with international structural codes?
What surface coating is best for cold storage facilities operating down to -30°C?
What is the standard lead time for wholesale factory orders shipped from China?
What is the allowable beam deflection limit for heavy-duty pallet racking?
How do safety back stoppers and wire mesh decking enhance warehouse safety?
Optimize Your Facility Capacity with Factory-Direct Engineering
Send us your warehouse floor plans, clear ceiling heights, pallet dimensions, and target weight requirements. Our structural engineers will generate a customized 2D/3D layout design and factory-direct wholesale quotation within 24 hours.
Get a Quote