Featured Industrial Pallet Racking Systems
Direct Factory Supply | Heavy-Duty Certified Structural Steel | International Quality Standards
Executive White Paper: Evaluating China's Pallet Racking Sourcing Landscape
Engineering Analysis, Structural Compliance, and Supply Chain ROI for Global Procurement Officers
In modern industrial logistics, selecting an optimal warehouse racking infrastructure directly dictates operational throughput, volumetric storage efficiency, and long-term capital expenditure safety. As global supply chains transition toward high-density automation and stringent safety protocols, China’s top pallet racking factories and wholesalers have evolved from low-cost material fabricators into sophisticated engineering partners capable of delivering complex, seismically engineered, and fully automated storage systems.
Navigating the Chinese manufacturing ecosystem requires a deep understanding of structural steel standards (such as Q235B, Q355B, and SS400 grade structural steel), cold-roll forming precision, electrostatic powder coating longevity, and compliance with international racking standards including ISO 9001, FEM 10.2.02 (European Federation of Materials Handling), RMI (Rack Manufacturers Institute), and ANSI MH16.1. This comprehensive technical analysis serves as a definitive procurement blueprint for supply chain managers, warehouse directors, and industrial contractors globally.
Comprehensive Racking Systems Architecture
Structural Comparison and Load Optimization Profiles
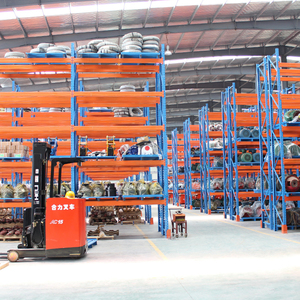
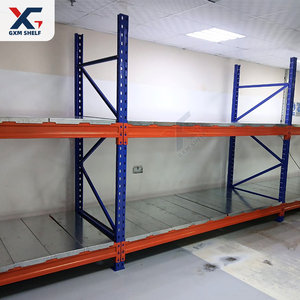
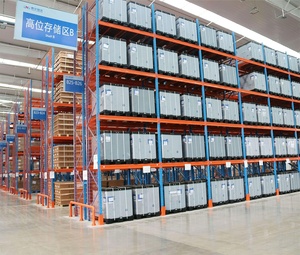
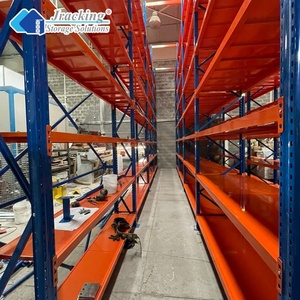
Selective Pallet Racking
The most versatile and widely implemented system globally. Engineered for 100% direct pallet access and seamless integration with standard counterbalance and reach forklifts. Features adjustable beam levels with boltless teardrop or diamond connection patterns.
Ideal For: High-SKU environments, 3PL logistics, FMCG distribution.
Drive-In & Drive-Through Racking
Designed for maximum volumetric storage by eliminating picking aisles. Forklifts drive directly into structural lanes to store pallets on continuous side rails. Operates on Last-In, First-Out (LIFO) or First-In, First-Out (FIFO) principles.
Ideal For: Cold storage, seasonal items, homogenous bulk cargo.
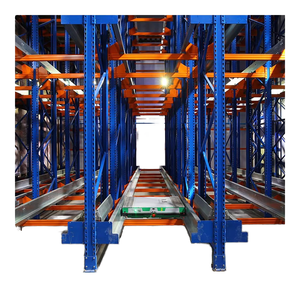
Radio Shuttle & 4-Way ASRS Systems
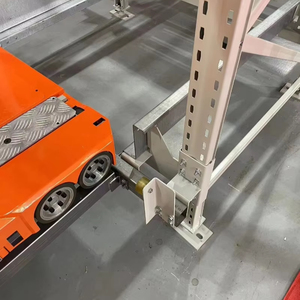
Semi-automated and fully automated high-density storage leveraging self-powered electric shuttles. Shuttles navigate inside deep storage channels controlled via Wi-Fi/WMS, dramatically reducing forklift travel time and risk of collision.
Ideal For: Smart warehouses, pharmaceutical, sub-zero cold rooms.
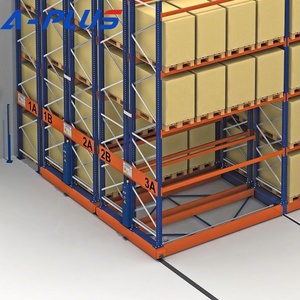
Motorized Electric Mobile Racking (MOVO)
Racking blocks mounted on heavy-duty motorized mobile bases running on embedded floor rails. Open picking aisles are created dynamically via remote control or touchscreens, effectively doubling warehouse storage capacity in the same footprint.
Ideal For: Expensive real estate, cold chain logistics, archival storage.
Very Narrow Aisle (VNA) Systems
Utilizes selective racking configured with ultra-narrow aisles (1.5m - 1.8m) and guided VNA trucks (wire or rail-guided). Maximizes vertical clear height up to 18 meters while retaining 100% individual pallet selectivity.
Ideal For: High-ceiling logistics hubs, order picking, e-commerce.
Heavy-Duty Cantilever Racking
Engineered with free-standing vertical columns and extended load arms without front upright obstructions. Purpose-built to handle long, bulky, or irregularly shaped industrial products with high structural rigidity.
Ideal For: Steel pipes, timber, aluminium profiles, sheet metal.
Engineering & Operational Performance Matrix
| Racking System Type | Selectivity % | Volumetric Density | Max Load Capacity / Level | Handling Equipment Required | Relative Cost Index |
|---|---|---|---|---|---|
| Selective Pallet Rack | 100% | 40% - 50% | up to 4,500 kg | Standard Reach / Counterbalance | Low (Baseline) |
| Drive-In Racking | 15% - 20% | 75% - 85% | up to 2,000 kg | Standard Reach Truck | Medium |
| Radio Shuttle System | 30% - 50% | 85% - 90% | up to 2,500 kg | Standard Forklift + Radio Cart | High (High ROI) |
| Very Narrow Aisle (VNA) | 100% | 65% - 75% | up to 3,500 kg | VNA Turret Truck / Articulated | Medium-High |
| Electric Mobile Racking | 100% | 85% - 95% | up to 8,000 kg/bay | Standard Reach Truck | High |
| 4-Way Shuttle ASRS | 100% (Automated) | 90% - 98% | up to 1,500 kg | Automated Elevator & Shuttle | Capital Intensive |
OEM/ODM Manufacturing Capabilities & Quality Assurance
Why Leading Global Enterprises Sourcing Racking from China
Leading Chinese racking manufacturers combine large-scale industrial output with rigorous structural engineering. The superiority of top-tier OEM/ODM factories lies in their end-to-end quality control pipeline, from raw material procurement to final surface passivation and export packaging.
Certified Raw Steel Sourcing & Metallurgical Compliance
Premier factories source exclusively from state-owned steel conglomerates (such as Baosteel, Shougang Group, and Ansteel). Steel coils undergo rigorous tensile testing, yield strength verification (Q235B vs Q355B), and chemical composition analysis. High-grade Q355B cold-rolled steel offers superior load-bearing characteristics with reduced structural deadweight, ensuring compliance with FEM 10.2.02 and RMI standards.
Precision Roll-Forming & Robotic Laser Welding
Advanced factories deploy multi-station continuous cold roll-forming lines capable of maintaining pitch tolerances within ±0.5mm over a 12-meter upright profile. Automated ABB and KUKA robotic welding cells guarantee 100% penetration welds on beam connectors and baseplates, eliminating human error and structural fatigue zones under cyclic dynamic loads.
Electrostatic Powder Coating & Surface Pre-treatment
To resist industrial abrasion and chemical degradation, components pass through a 9-stage automatic pre-treatment process involving degreasing, zinc phosphating, and deionized water rinsing. The electrostatically applied thermosetting epoxy-polyester powder coat is cured at 200°C, delivering salt-spray corrosion resistance exceeding 500 hours for humid or cold-room environments.
Finite Element Analysis (FEA) & Seismic Structural Engineering
In-house engineering teams utilize ANSYS and SAP2000 FEA simulation software to model stress distribution, deflection, and buckling behavior under static and dynamic loading. Custom structural designs can be engineered to resist severe earthquake forces (up to Zone 4 / Richter Scale 8.0) using heavy-duty baseplates, expansion anchors, and dynamic vertical sway bracing.
Information Gain Insight: Custom OEM/ODM Protocol
When sourcing custom pallet racking from China, request a complete Structural Engineering Verification Report detailing buckling factors, safety coefficient ratios (typically 1.5 to 1.95 under EN 15512), mill test certificates (MTC), and 3D DWG/BIM model integration prior to mass production.
Future Procurement Trends in Industrial Storage
Strategic Evolution Toward Smart Automation and Sustainable Materials
The global warehousing market is undergoing a structural transition driven by e-commerce acceleration, labor cost escalation, and corporate ESG (Environmental, Social, and Governance) mandates. Chinese racking manufacturers are at the forefront of these technological shifts:
1. Integration with ASRS & Autonomous Mobile Robots (AMRs)
Traditional static racking is rapidly giving way to robot-compatible structures. Future procurement favors rack systems with ultra-precise beam leveling tolerances (±1.0mm) to accommodate high-speed ASRS stacker cranes, AGVs, and 3D shuttle fleets.
2. Green Supply Chain & Low-Carbon Steel
Leading Chinese exporters are implementing carbon-neutral manufacturing initiatives. By leveraging scrap-recycled electric arc furnace (EAF) steel and zero-emission powder coatings, suppliers help overseas buyers meet strict Scope 3 decarbonization targets.
3. Modular Expandability & IoT Rack Monitoring
Modern racking installations now feature embedded IoT load sensors and shock detectors. These smart components transmit real-time data regarding beam deflection, impact events, and overload warnings directly to warehouse management dashboards.
Procurement FAQ: Sourcing Pallet Racking from China
Expert Answers to Critical Engineering, Logistics, and Commercial Queries
Optimize Your Warehouse Footprint Today
Connect with China’s premier racking engineering team for custom 3D CAD layouts, structural calculations, and factory-direct wholesale pricing.